Ceramic Clipper Blade Manufacturer: OEM Specs, MOQ & Cost
What to specify when sourcing zirconia ceramic clipper blades: 3Y-TZP grades, HV 1200-1400 hardness, CIM tooling cost, 500-2,000 MOQ and $2.80-6.50 FOB pricing. Written by a blade factory. Get a quote.
Quick answer: A genuine ceramic clipper blade manufacturer sinters yttria-stabilised zirconia (3Y-TZP) into the moving blade only — the stationary comb stays steel. Specify the grade (3Y-TZP for toughness, 5Y-PSZ only if you accept lower strength), Vickers hardness HV 1,200-1,400 per ASTM C1327, flexural strength above 900 MPa per ASTM C1161, and cutting-edge flatness within 0.01mm. Expect 500-2,000 piece MOQ, $3,000-8,000 for ceramic injection moulding tooling, 45-70 day first-run lead time, and $2.80-6.50 FOB China per ceramic moving blade depending on size and volume.
We manufacture both steel and zirconia blades in the same plant in Haining, Zhejiang. This guide is written for the person on the other side of the RFQ — a clipper brand, a grooming distributor, or a private-label buyer who has been quoted "ceramic blades" by four factories at four different prices and has no way to tell which quote is real. If you want the end-user comparison instead, read ceramic vs steel clipper blades.
First Rule: Ceramic Is a Moving-Blade Material, Not a Blade-Set Material
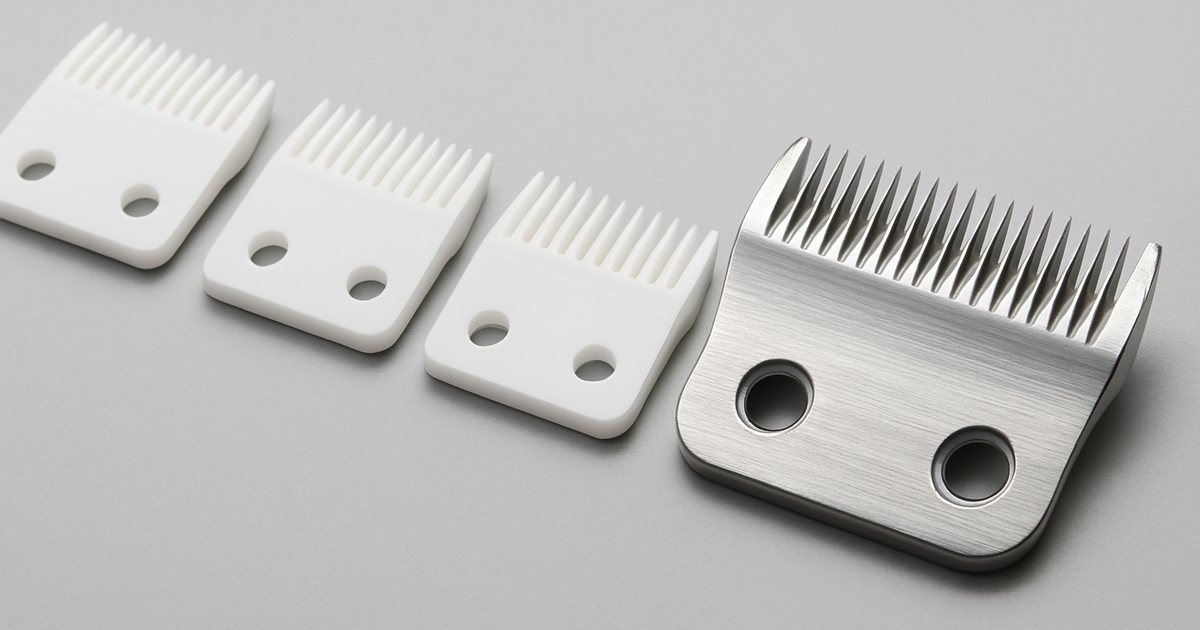
Almost every "ceramic blade" sold at retail is a hybrid: a zirconia moving (cutter) blade riding on a hardened steel stationary (comb) blade. This is not cost-cutting. It is a design constraint.
The stationary blade carries the mounting screws, absorbs drop impact, and takes the spring tension load. Zirconia has excellent compressive strength but low tolerance for point loading around a screw hole — a torqued fastener in a ceramic comb is a crack initiator. The moving blade, by contrast, sees mostly sliding contact, which is exactly where zirconia's hardness and low friction pay off.
If a supplier offers you a fully ceramic blade set at a normal price, ask to see the stationary blade in the hand. Nine times out of ten it is a steel comb with a white coating, and you are being quoted on a marketing description rather than a bill of materials.
Zirconia Grades: What You Are Actually Buying
"Ceramic" is not a specification. There are three materials in common use for grooming blades, and their prices differ by more than 2x.
| Material | Vickers hardness | Flexural strength | Fracture toughness | Verdict for clipper blades |
|---|---|---|---|---|
| 3Y-TZP zirconia | HV 1,200-1,400 | 900-1,200 MPa | 5-10 MPa·m1/2 | Correct choice — best strength-to-hardness balance |
| 5Y-PSZ zirconia | HV 1,250-1,350 | 550-750 MPa | 2.2-3.5 MPa·m1/2 | Cheaper feedstock, noticeably more chip-prone at the tooth tip |
| Alumina (Al2O3 99%) | HV 1,500-1,800 | 300-400 MPa | 3-4 MPa·m1/2 | Harder but brittle — avoid for fine tooth profiles |
| 440C stainless (reference) | HV 620-750 (HRC 58-62) | n/a (ductile) | ~25 MPa·m1/2 | Tougher, but wears 3-5x faster |
3Y-TZP means zirconia stabilised with roughly 3 mol% yttria. It is the same material family qualified for surgical implants under ISO 13356, which is a useful reference point when you write a spec: a supplier who cannot tell you the yttria content and grain size of their powder is buying pre-mixed feedstock and reselling it, not engineering it.
Grain size matters more than most buyers realise. Below roughly 0.5 µm the material holds a finer edge and resists chipping; above about 1 µm you gain hardness on paper but lose the transformation toughening that keeps a tooth tip intact when it hits a matted knot.
How Ceramic Clipper Blades Are Actually Made
The process is ceramic injection moulding (CIM) — the same family as the MIM process we use for steel blades, with a ceramic feedstock and a very different sintering curve.
| Step | What happens | What can go wrong |
|---|---|---|
| 1. Feedstock | 3Y-TZP powder compounded with polymer binder, granulated to 50-150 µm | Batch-to-batch yttria variation; agglomerates become sinter voids |
| 2. Injection | Green part moulded oversize to compensate shrinkage | Weld lines across a tooth root — invisible until it snaps in the field |
| 3. Debinding | Solvent and thermal binder removal over 12-30 hours | Rushing this stage blisters or cracks the part internally |
| 4. Sintering | 1,400-1,450°C; part shrinks roughly 20-22% linearly to >99% theoretical density | Uneven furnace loading gives non-uniform shrinkage and warped blades |
| 5. Diamond grinding | Cutting edge and seating face ground with resin-bond diamond wheels | The single biggest cost driver — nothing but diamond touches sintered zirconia |
| 6. Lapping and inspection | Face lapped flat, edge honed, 100% visual under magnification | Micro-chips under 50 µm skipped by unmagnified inspection |
That 20-22% shrinkage is why ceramic tooling is expensive and why a first article takes so long. The mould is not cut to the blade drawing; it is cut to the drawing scaled up by the measured shrink factor of that specific feedstock lot, then corrected after the first sintered samples come off. Budget two tooling correction rounds. A factory that promises a first-article match in one round has either done this exact geometry before or is not being straight with you.
The Spec Sheet You Should Send With Your RFQ
Most ceramic blade RFQs we receive say "ceramic blade, A5 #10, please quote". Here is what a specification that produces comparable quotes actually contains.
| Parameter | Specify | Test method |
|---|---|---|
| Material | 3Y-TZP, yttria 4.5-5.5 wt%, grain size <0.5 µm | Supplier powder certificate + SEM on request |
| Density | ≥6.00 g/cm³ (≥99% theoretical) | Archimedes, ASTM C373 |
| Hardness | HV10 ≥1,200 | ASTM C1327 |
| Flexural strength | ≥900 MPa | ASTM C1161, 4-point |
| Edge flatness | ≤0.01mm across cutting edge | Optical flat / profilometer |
| Tooth pitch tolerance | ±0.03mm | Vision measurement, 5 pcs/lot |
| Edge chip limit | No chip >0.05mm; zero chips on tooth tips | 30x magnification, 100% inspection |
| Mating steel comb | 420J2 or 440C, HRC 58-62, matched lapped pair | Rockwell, per steel grade spec |
| Assembled heat rise | ≤45°C blade surface after 30 min continuous run | IR thermometer, ambient 25°C |
The last line is the one that separates a real ceramic advantage from a cosmetic one. Zirconia conducts heat at roughly 2-3 W/m·K against 24-26 W/m·K for martensitic stainless. That difference is what produces the cool-running behaviour groomers care about — but only if the blade pair is properly lapped. A poorly mated ceramic blade generates more friction heat than a well-mated steel one, and the ceramic then refuses to conduct it away. If you are chasing that benefit specifically, see why clipper blades get hot.
MOQ, Tooling and FOB Pricing
| Scenario | MOQ | Tooling | Lead time | FOB China / pc |
|---|---|---|---|---|
| Existing A5 size, your logo on packaging | 500 pcs | None | 25-35 days | $4.20-6.50 |
| Existing size, laser-marked blade + custom box | 1,000 pcs | $200-600 (marking + carton) | 35-45 days | $3.80-5.60 |
| New tooth geometry, new CIM mould | 3,000-5,000 pcs | $3,000-8,000 | 55-70 days | $3.20-5.00 |
| Repeat order, established SKU, 10,000+ pcs | 2,000 pcs | Amortised | 25-30 days | $2.80-4.20 |
Prices above are for the ceramic moving blade alone. A complete hybrid set — ceramic cutter plus lapped steel comb, springs, and screws — typically runs $6.00-12.00 FOB depending on size and packaging. As a rule of thumb, ceramic costs 2.2-3.5x the equivalent all-steel set at the factory gate, and that multiple narrows as volume rises because diamond grinding time, not material, dominates the cost.
Quality Control: The Four Tests That Catch Real Defects
Ceramic fails differently from steel. Steel blades dull; ceramic blades chip. Your inspection plan has to reflect that.
- Magnified edge inspection (30x, 100% of units). Non-negotiable. A 40 µm tooth-tip chip is invisible to the naked eye and will pull hair on the first client. Ask whether inspection is 100% or AQL-sampled — for ceramic we run 100% and it is a real cost line.
- Drop test, 1.0m onto hardwood, 3 orientations. Ceramic that survives a 1.0m drop onto wood is normal; ceramic that survives 1.5m onto concrete does not exist. Set the acceptance criterion where physics allows, then put the real limit on the packaging.
- Cut-and-heat run, 30 minutes continuous. Measures the mating quality of the pair, not just the ceramic. Record surface temperature at 10, 20 and 30 minutes.
- Hydrothermal ageing check (only if steam sterilisation is in scope). 3Y-TZP is subject to low-temperature degradation in hot, humid conditions — a known behaviour of the material, which is why ISO 13356 includes an accelerated ageing requirement. For veterinary customers who autoclave, specify an aged-strength retention criterion. For barbershop use with spray disinfectant, it is not a practical concern.
Six Red Flags When Auditing a "Ceramic Blade Manufacturer"
- No sintering furnaces on site. Ask to see them. Many suppliers buy sintered blanks and only grind, which is a legitimate business — but it means they cannot control density, grain size or shrinkage, and they cannot fix a material problem when it appears.
- No diamond grinding equipment. Same logic in reverse. If they neither sinter nor grind, they are a trading company.
- A quote that does not change when you change the grade. 3Y-TZP and 5Y-PSZ feedstock differ meaningfully in cost. Identical pricing means they are not selecting the material.
- No shrinkage compensation discussion during tooling review. If nobody mentions the shrink factor, they have not built a ceramic mould before.
- Retail-grade claims with no test data. "5x longer life" should be backed by a documented cutting test protocol. Ours is run against a matched 440C control on the same clipper, same coat type, edge-life measured to a defined pull-force threshold.
- An offer to make the stationary comb in ceramic too. See the first section. This tells you they are selling a story.
Compliance and Documentation for Export
The blade itself is a passive metal/ceramic component, so most regulatory burden sits on the finished appliance rather than on your blade order. Even so, buyers should collect the following at PO stage so the finished-goods file is complete: RoHS and REACH declarations covering the blade, the packaging and any oil supplied with it; a material certificate naming the zirconia grade and powder supplier; ISO 9001 certification for the plant; and, where the blade contacts skin in prolonged use, a nickel-release statement for the steel comb under EN 1811 / REACH Annex XVII entry 27.
If your finished clipper carries a CE mark, the relevant appliance safety standard is IEC/EN 60335-2-8 for shavers, hair clippers and similar appliances — your blade supplier's documents feed that file but do not replace it.
Working With Us
We sinter and grind zirconia in-house alongside our steel lines, which means one supplier for a hybrid programme and one set of matched tolerances between cutter and comb. Our ceramic moving blades cover #3F through #40 as drop-in replacements for standard A5 blade sets, MOQ from 500 pieces. For programme structure, pricing tiers and private-label packaging, see our OEM & custom manufacturing page or send us your drawing for a quote.
Related Guides
- Ceramic vs Steel Clipper Blades — the end-user comparison: edge life, heat, cost of ownership.
- Ceramic Pet Grooming Blades — why groomers switch, with measured temperature data.
- Clipper Blade Materials Compared — ceramic against the full steel range.
- How to Source OEM Clipper Blades from China — the wider sourcing process, payment terms and factory audits.
- Top Clipper Blade Manufacturers in China — verified factory list with capability notes.
Frequently Asked Questions
What material are ceramic clipper blades made of?
Professional ceramic clipper blades are made from yttria-stabilised zirconia, usually 3Y-TZP — zirconium dioxide stabilised with about 3 mol% yttria. It reaches HV 1,200-1,400 Vickers hardness and 900-1,200 MPa flexural strength after sintering at 1,400-1,450°C. Alumina is harder but too brittle for fine tooth profiles, and 5Y-PSZ is cheaper but chips more readily at the tooth tip.
Why is the stationary blade still steel on a ceramic blade set?
The stationary comb carries mounting screws, spring tension and drop impact. Zirconia tolerates compression well but cracks under point loading around a fastener hole, so a torqued screw in a ceramic comb becomes a crack initiator. Every credible ceramic blade set is a hybrid: zirconia moving blade on a hardened stainless stationary blade.
What is the MOQ for OEM ceramic clipper blades?
500 pieces for an existing size with your branding on the packaging, 1,000 pieces if the blade itself is laser-marked, and 3,000-5,000 pieces when a new ceramic injection moulding tool is required. Repeat orders on an established SKU can drop back to 2,000 pieces.
How much do ceramic clipper blades cost from a factory?
$2.80-6.50 FOB China per ceramic moving blade depending on size, volume and branding, or $6.00-12.00 for a complete hybrid set with steel comb, springs and screws. Ceramic runs 2.2-3.5x an equivalent all-steel set because diamond grinding and lapping, not raw material, dominate the cost.
How long does ceramic blade tooling take?
55-70 days for a first production run on new tooling. The ceramic injection mould must be cut oversize to compensate for 20-22% linear sintering shrinkage, then corrected after first sintered samples are measured. Budget two correction rounds; a supplier promising a first-article match in one round has either run that exact geometry before or is understating the work.
Do ceramic clipper blades really last 5x longer than steel?
In matched testing against a 440C control on the same clipper and coat type, zirconia holds its edge roughly 3-5x longer, because at HV 1,200+ it is far harder than the HV 620-750 of hardened stainless. The caveat is failure mode: steel dulls gradually and can be resharpened, while ceramic stays sharp and then chips. Ceramic blades cannot be sharpened at home and should be replaced rather than reground.
Can ceramic clipper blades be sterilised in an autoclave?
Zirconia itself handles autoclave temperatures, but 3Y-TZP is subject to low-temperature hydrothermal degradation under repeated hot humid cycling — the reason ISO 13356 includes an accelerated ageing test for implant-grade zirconia. For veterinary customers who autoclave routinely, write an aged-strength retention requirement into the specification. For barbershop and salon use with spray disinfectant, it is not a practical concern.