Stainless Steel Clipper Blade Manufacturer: 440C, MOQ & Cost
Sourcing stainless steel clipper blades? 440C vs 420J2 grades, HRC 58-62, 0.005mm flatness, 500 pc MOQ and $0.35-7.00 FOB pricing from a factory since 2004. Get a quote.
Quick answer: When you source from a stainless steel clipper blade manufacturer, "stainless steel" tells you almost nothing. Specify the grade (440C / Chinese 9Cr18 or 9Cr18Mo for professional blades, 420J2 / 3Cr13 only for consumer trimmers), hardness of HRC 58-62 verified by Vickers or superficial Rockwell on the tooth area, vacuum hardening plus sub-zero treatment, mating-face flatness within 0.005mm, and passivation per ASTM A967. Expect a 500-piece MOQ on existing sizes, $1,500-10,000 tooling for a new blade, 25-60 day lead times, and $0.35-7.00 FOB China per blade set depending on type, forming method and volume.
We have made clipper and trimmer blades in Haining, Zhejiang since 2004 — stamped, fine-blanked and metal-injection-moulded, in stainless steel and zirconia. This guide is written for the buyer on the other side of the RFQ: a clipper brand, a barber or grooming distributor, or a private-label seller comparing four quotes that all say "premium stainless steel" and differ by 3x in price. If you want the end-user explanation of steel grades instead, read clipper blade steel grades explained.
"Stainless Steel" Is Not a Specification: The Grades You Will Actually Be Quoted
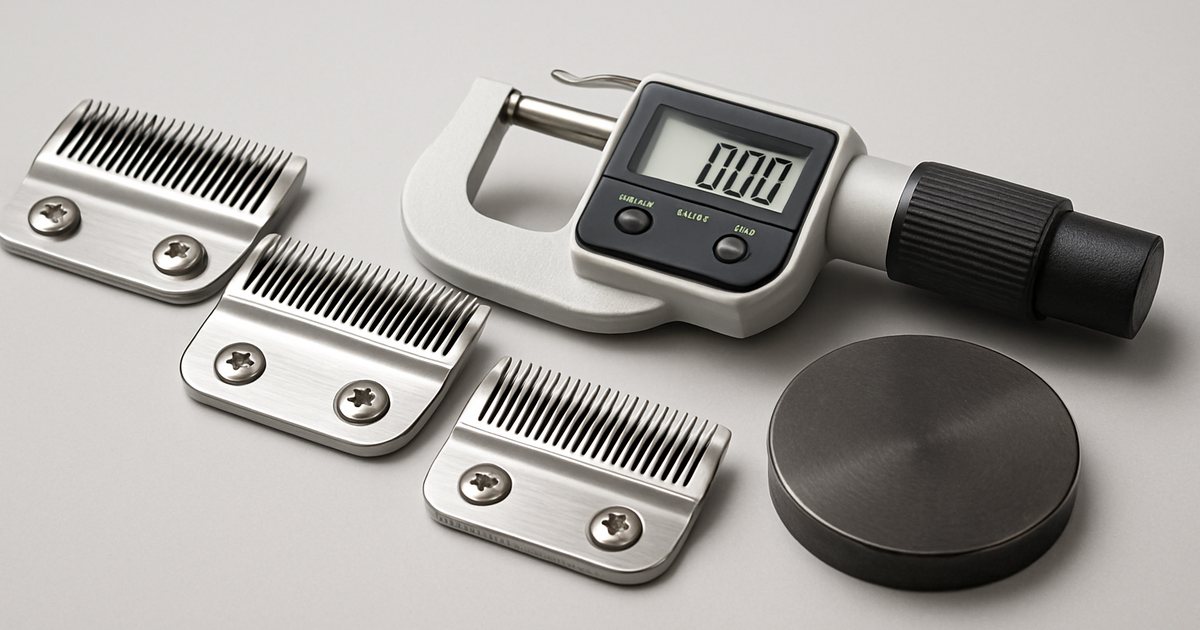
Chinese factories write their quote sheets in GB/T 1220 designations, while your spec sheet probably says AISI or JIS. Most buyers never connect the two, so a "4Cr13 blade" and a "9Cr18 blade" look like the same product on paper. They are not. The number in front of "Cr" is the carbon content in hundredths of a percent, and carbon is what decides how hard the edge can get.
| China (GB/T 1220) | AISI / JIS equivalent | Carbon % | Chromium % | Achievable HRC | Where it belongs |
|---|---|---|---|---|---|
| 3Cr13 | 420J2 / SUS420J2 | 0.26-0.35 | 12-14 | 50-53 | Consumer trimmers, nose trimmers, retail under $30 |
| 4Cr13 | 420 (high-carbon variant) | 0.36-0.45 | 12-14 | 52-55 | Entry-level barber blades, household clippers |
| 7Cr17 | 440A / SUS440A | 0.60-0.75 | 16-18 | 55-57 | Mid-range professional, humid-market blades |
| 9Cr18 / 9Cr18Mo | 440C / SUS440C | 0.90-1.10 | 16-19 | 58-62 | Professional barber, A5 detachable, pet grooming |
| 9Cr18MoV | 440C + vanadium (close to AUS-8 class) | 0.85-0.95 | 17-19 | 58-61 | Premium blades where edge wear is the complaint |
Two practical consequences. First, the price gap between 3Cr13 and 9Cr18 sheet is small — perhaps $0.03-0.08 per blade in material — so a large price difference between two "stainless" quotes is rarely explained by steel. It is explained by heat treatment and grinding, which we cover below. Second, a quote that names no grade at all almost always means 3Cr13 or 4Cr13. A factory running 440C says so, because it is a selling point.
Two Ways to Form a Steel Blade: Stamping vs Metal Injection Moulding
The second decision hidden inside every quote is how the blade blank was formed. It drives tooling cost, MOQ and the tolerance you can hold on the teeth.
| Property | Stamped / fine-blanked sheet | MIM (metal injection moulding) |
|---|---|---|
| Typical blank tolerance | ±0.1mm (±0.02-0.05mm fine-blanked) | ±0.03-0.05mm |
| Typical finished hardness | HRC 55-58 | HRC 60-62 |
| Material waste | 20-40% (skeleton scrap) | Under 3% |
| Geometry limits | Flat parts, uniform thickness | Stepped thickness, integrated bosses, curved tooth roots |
| New tooling cost | $1,500-4,000 (progressive die) | $4,000-10,000 (multi-cavity mould) |
| Tooling lead time | 3-4 weeks | 4-6 weeks |
| Sensible MOQ on new tooling | 2,000-3,000 pcs | 5,000 pcs |
| Best for | T-blades, trimmer blades, simple flat combs | A5 detachable blades, complex stationary blades |
Neither route is "better" in the abstract. A flat T-blade trimmer set is a stamping job, and paying for MIM tooling on it is wasted money. A detachable A5 blade with a stepped heel, latch pocket and curved tooth roots is where MIM earns its mould cost, because the alternative is stamping plus three machining operations. Our A5 range is moulded from gas-atomised 440C powder at 5-15µm particle size — the full sequence is in how clipper blades are made with MIM, and the cost trade-off is broken down in MIM vs CNC machining cost.
Heat Treatment: Where Cheap Blades Are Really Made Cheap
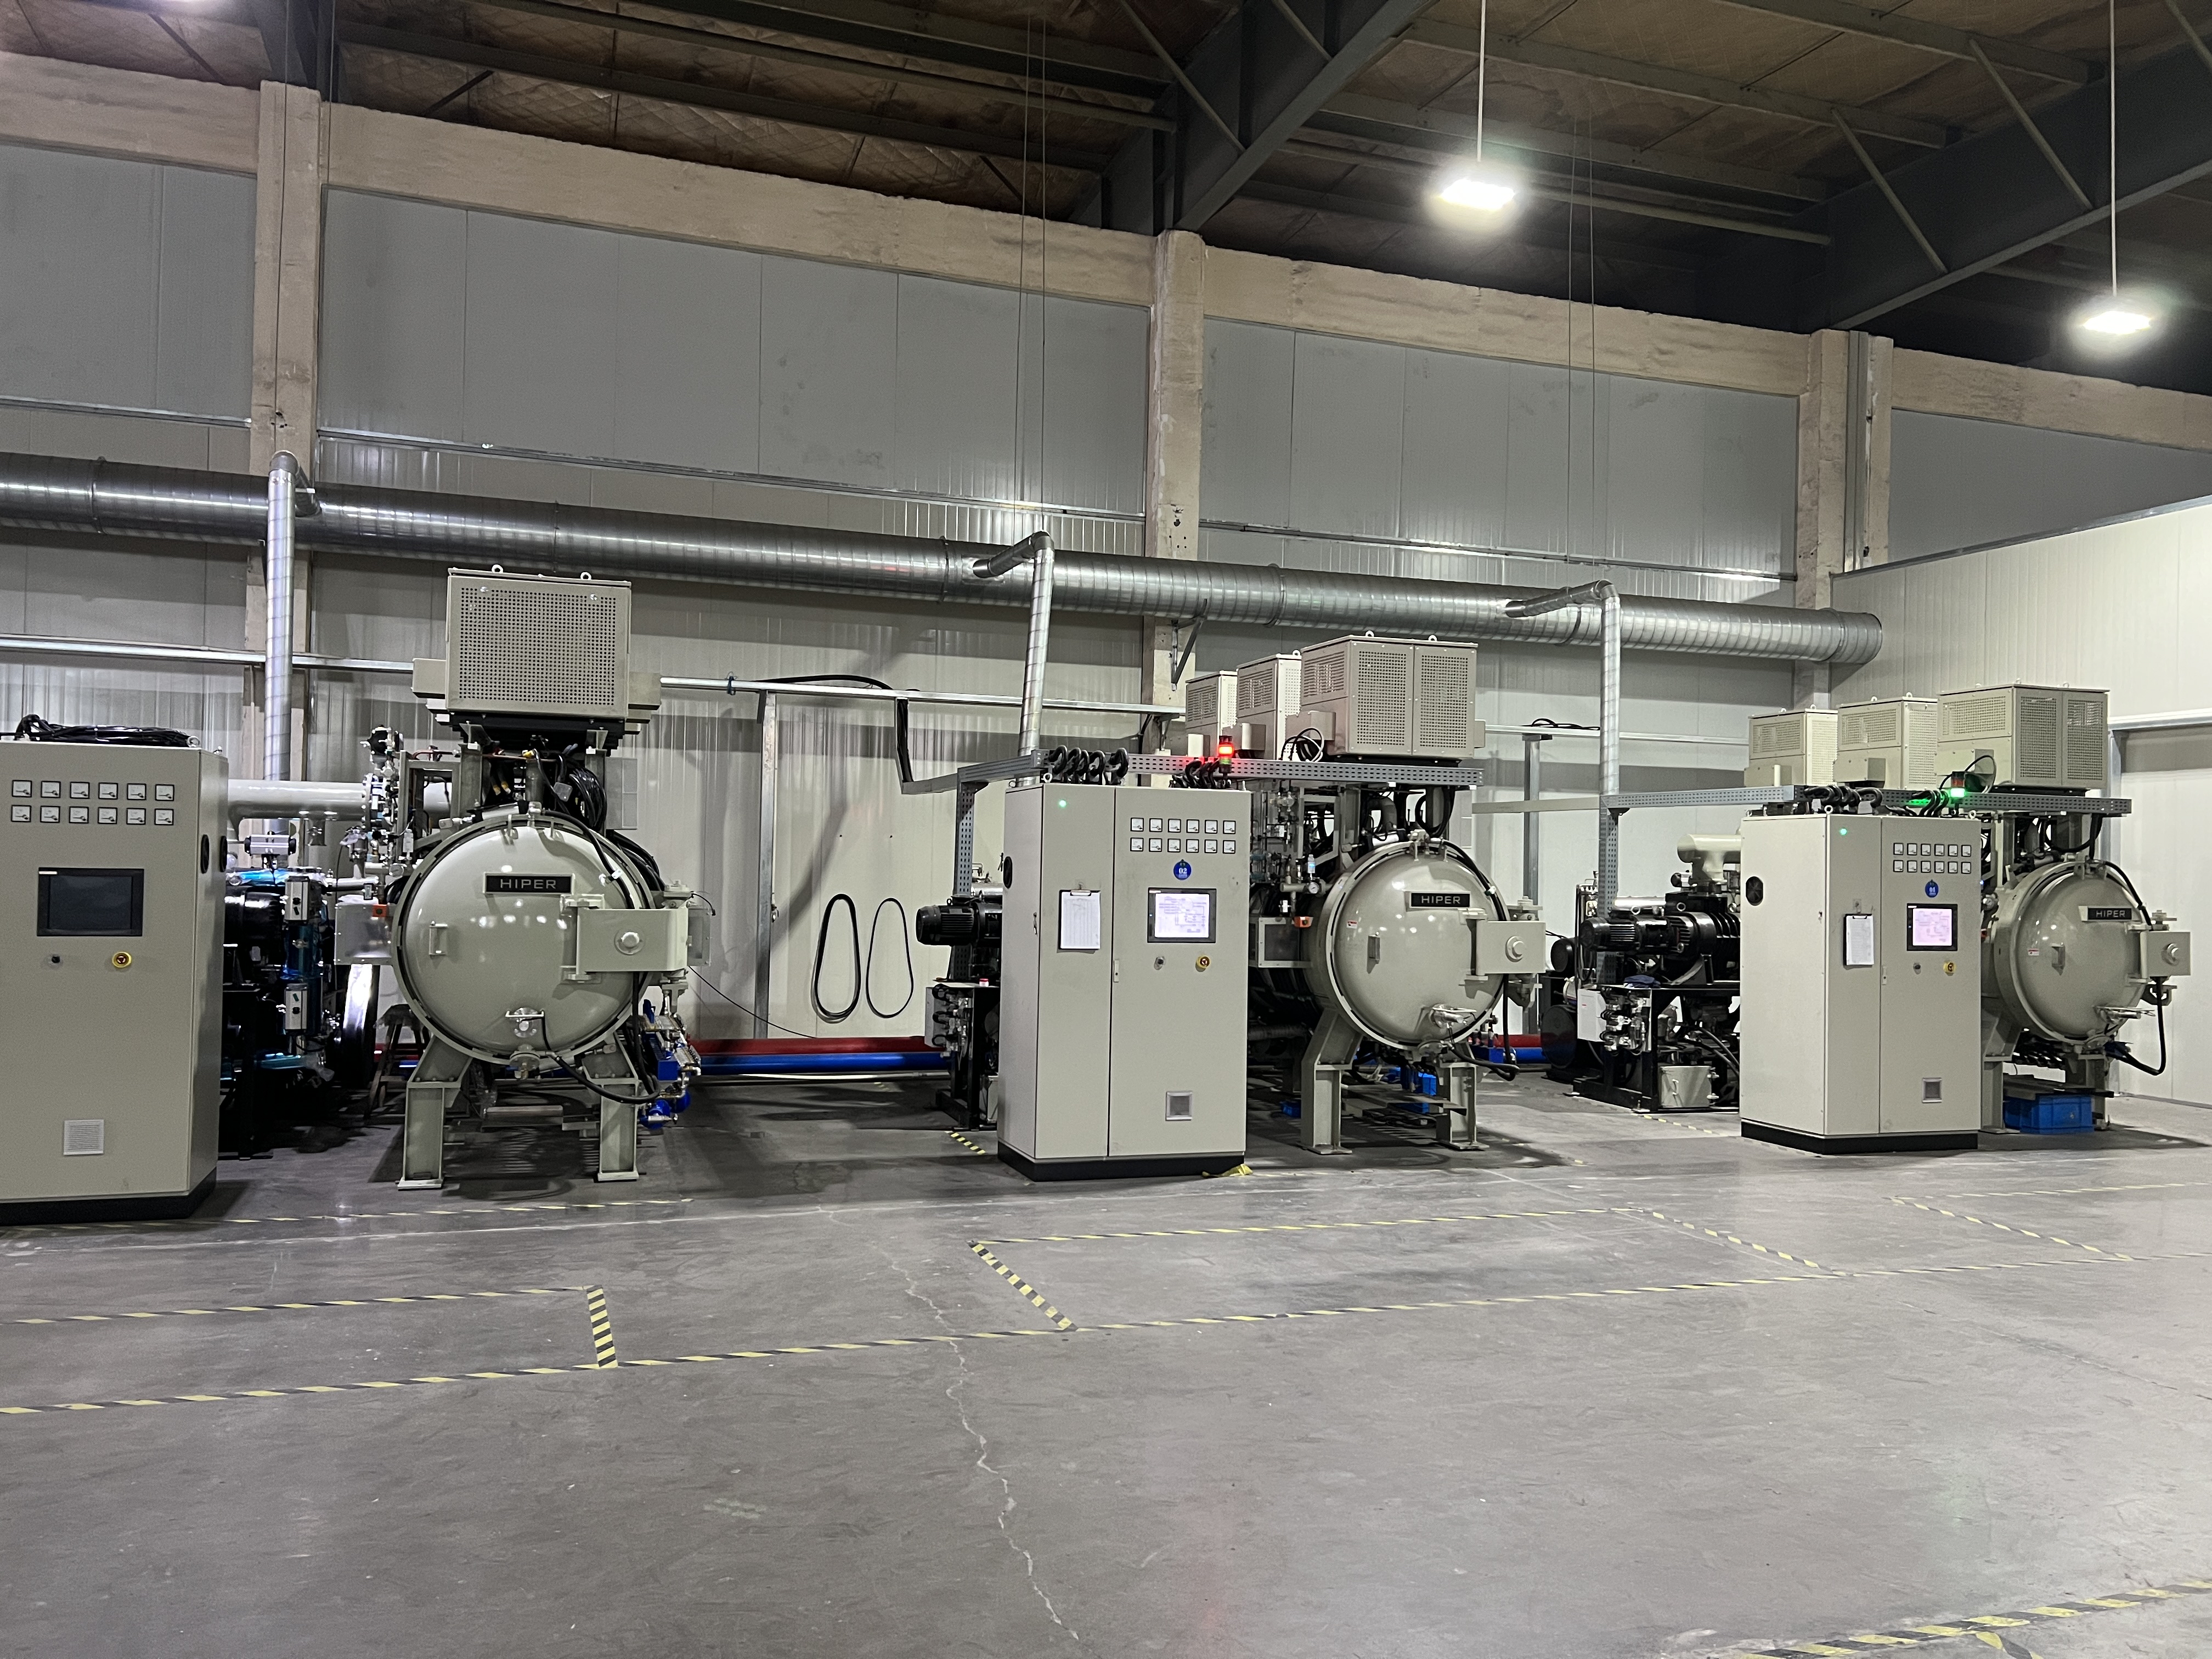
Give two factories the same 440C sheet and you can get blades four HRC points apart. The steel sets the ceiling; heat treatment decides how close you get to it. A correct cycle for a martensitic stainless blade looks like this:
- Vacuum hardening at 1,030-1,070°C, followed by high-pressure gas quench. Vacuum matters because it prevents surface decarburisation.
- Sub-zero treatment at -70 to -80°C within a few hours of quenching. 440C retains a meaningful fraction of soft austenite after quench; cooling below zero converts much of it to martensite, adding roughly 1-2 HRC and improving dimensional stability.
- Double temper at 150-200°C. Low tempering keeps hardness near the top of the range. Tempering higher trades hardness for toughness — acceptable for livestock combs, wrong for a finishing blade.
The cheap alternative is a mesh-belt atmosphere furnace with no sub-zero step. It is faster and costs a fraction as much per piece, but poor atmosphere control leaves a decarburised skin of roughly 0.02-0.05mm. On a thick part that would not matter. On a clipper tooth, that soft skin is the cutting edge — the blade feels sharp out of the box, then dulls within weeks and never recovers after its first regrind.
Grinding and Lapping: The Numbers That Decide How a Blade Cuts
Hair is cut by shear between two surfaces. Once hardness is right, cutting quality comes down to how well those two surfaces meet — and that is a grinding and lapping question, not a steel question. These are the dimensions we control on every blade pair, and what happens when they drift:
| Dimension | Our target | Failure if out of spec |
|---|---|---|
| Mating-face flatness (each blade) | ≤ 0.005mm over the tooth zone | Hair folds between blades instead of shearing ("pulling") |
| Lapped-face roughness | Ra ≤ 0.2µm | Heat build-up, faster wear, gritty feel on the lever |
| Tooth pitch tolerance | ±0.02mm | Uneven cut line, "tramlines" on short fades |
| Edge straightness across teeth | ≤ 0.01mm | One corner cuts, the other skips |
| Moving-blade set-back (barber T-blade) | 0.2-0.8mm, per design | Too little: skin nicks. Too much: blade will not cut close |
| Spring / tension load | Specified per model, ±10% | Too high: heat. Too low: hair chewing and noise |
Flatness is the one to watch. A 0.005mm tolerance is five microns — about a tenth of a human hair's diameter — and it cannot be verified with calipers. Ask how the factory checks it: an optical flat, a granite surface plate with a 0.005mm feeler, or a coordinate measuring machine are all credible answers. "We check by hand" is not. For set-back and zero-gap adjustment on barber blades, see zero-gap clipper blades explained.
The Spec Sheet to Send With Your RFQ
Copy this into your RFQ. A factory that cannot quote against it line by line is telling you something useful before you pay for samples.
| Line | Requirement | Verification |
|---|---|---|
| 1. Material | SUS440C / 9Cr18Mo (or 420J2 / 3Cr13 for consumer SKUs) | Mill certificate per heat lot |
| 2. Hardness | HRC 58-62 equivalent (HV 650-750) | Vickers per ASTM E384, 5 pcs per lot |
| 3. Heat treatment | Vacuum hardening + sub-zero + double temper | Furnace chart per batch |
| 4. Flatness | ≤ 0.005mm on mating faces | Optical flat or CMM, 10 pcs per lot |
| 5. Surface finish | Ra ≤ 0.2µm lapped face | Profilometer, first article |
| 6. Tooth geometry | Pitch ±0.02mm, per drawing | Optical projector, first article + AQL |
| 7. Passivation | Per ASTM A967 (nitric or citric) | Process record |
| 8. Corrosion | No red rust after 24h neutral salt spray | ASTM B117 / ISO 9227, 3 pcs per lot |
| 9. Fit | Fits named host clippers without shims | Fit test on 3 host models |
| 10. Packaging | VCI anti-rust bag or oil film, blade guard | Visual, AQL |
Line 8 deserves a note. 440C has lower corrosion resistance than 420J2 because more of its chromium is tied up in carbides. That is the price of hardness, and it is why passivation and packaging matter more for a professional blade than a cheap one. For EU-bound skin-contact products, also ask for nickel-release data to EN 1811 against the REACH Annex XVII limit of 0.5 µg/cm²/week. Martensitic grades carry little nickel and normally pass comfortably, but the test report is what your importer will ask for. If rust complaints are already reaching you from the field, our clipper blade rust guide explains the usual causes.
MOQ, Tooling, Lead Time and FOB Pricing
| Blade type | Typical grade / route | MOQ (existing size) | Lead time | FOB China / set |
|---|---|---|---|---|
| Consumer trimmer / nose trimmer blade | 420J2, stamped | 1,000 pcs | 20-30 days | $0.35-0.80 |
| Barber T-blade / taper blade set | 440C, stamped + ground | 500 pcs | 25-35 days | $0.90-2.20 |
| A5 detachable blade (#3F-#40) | 440C, MIM | 500 pcs per size | 25-35 days | $1.90-3.80 |
| Wide / livestock comb and cutter | 440C or tool steel, MIM or forged | 500 pcs | 30-40 days | $3.50-7.00 |
| New geometry on new tooling | Any | 2,000-5,000 pcs | 50-60 days incl. tooling | Quoted per drawing |
Laser-marking your logo on the blade adds roughly $0.03-0.08 per piece and moves the MOQ to 1,000. Retail blister or boxed packaging adds $0.15-0.60 depending on format. If you are building a brand rather than buying a single part, our private label programme bundles blade, packaging and inserts into one quote.
Quality Control: Five Tests That Catch Real Defects
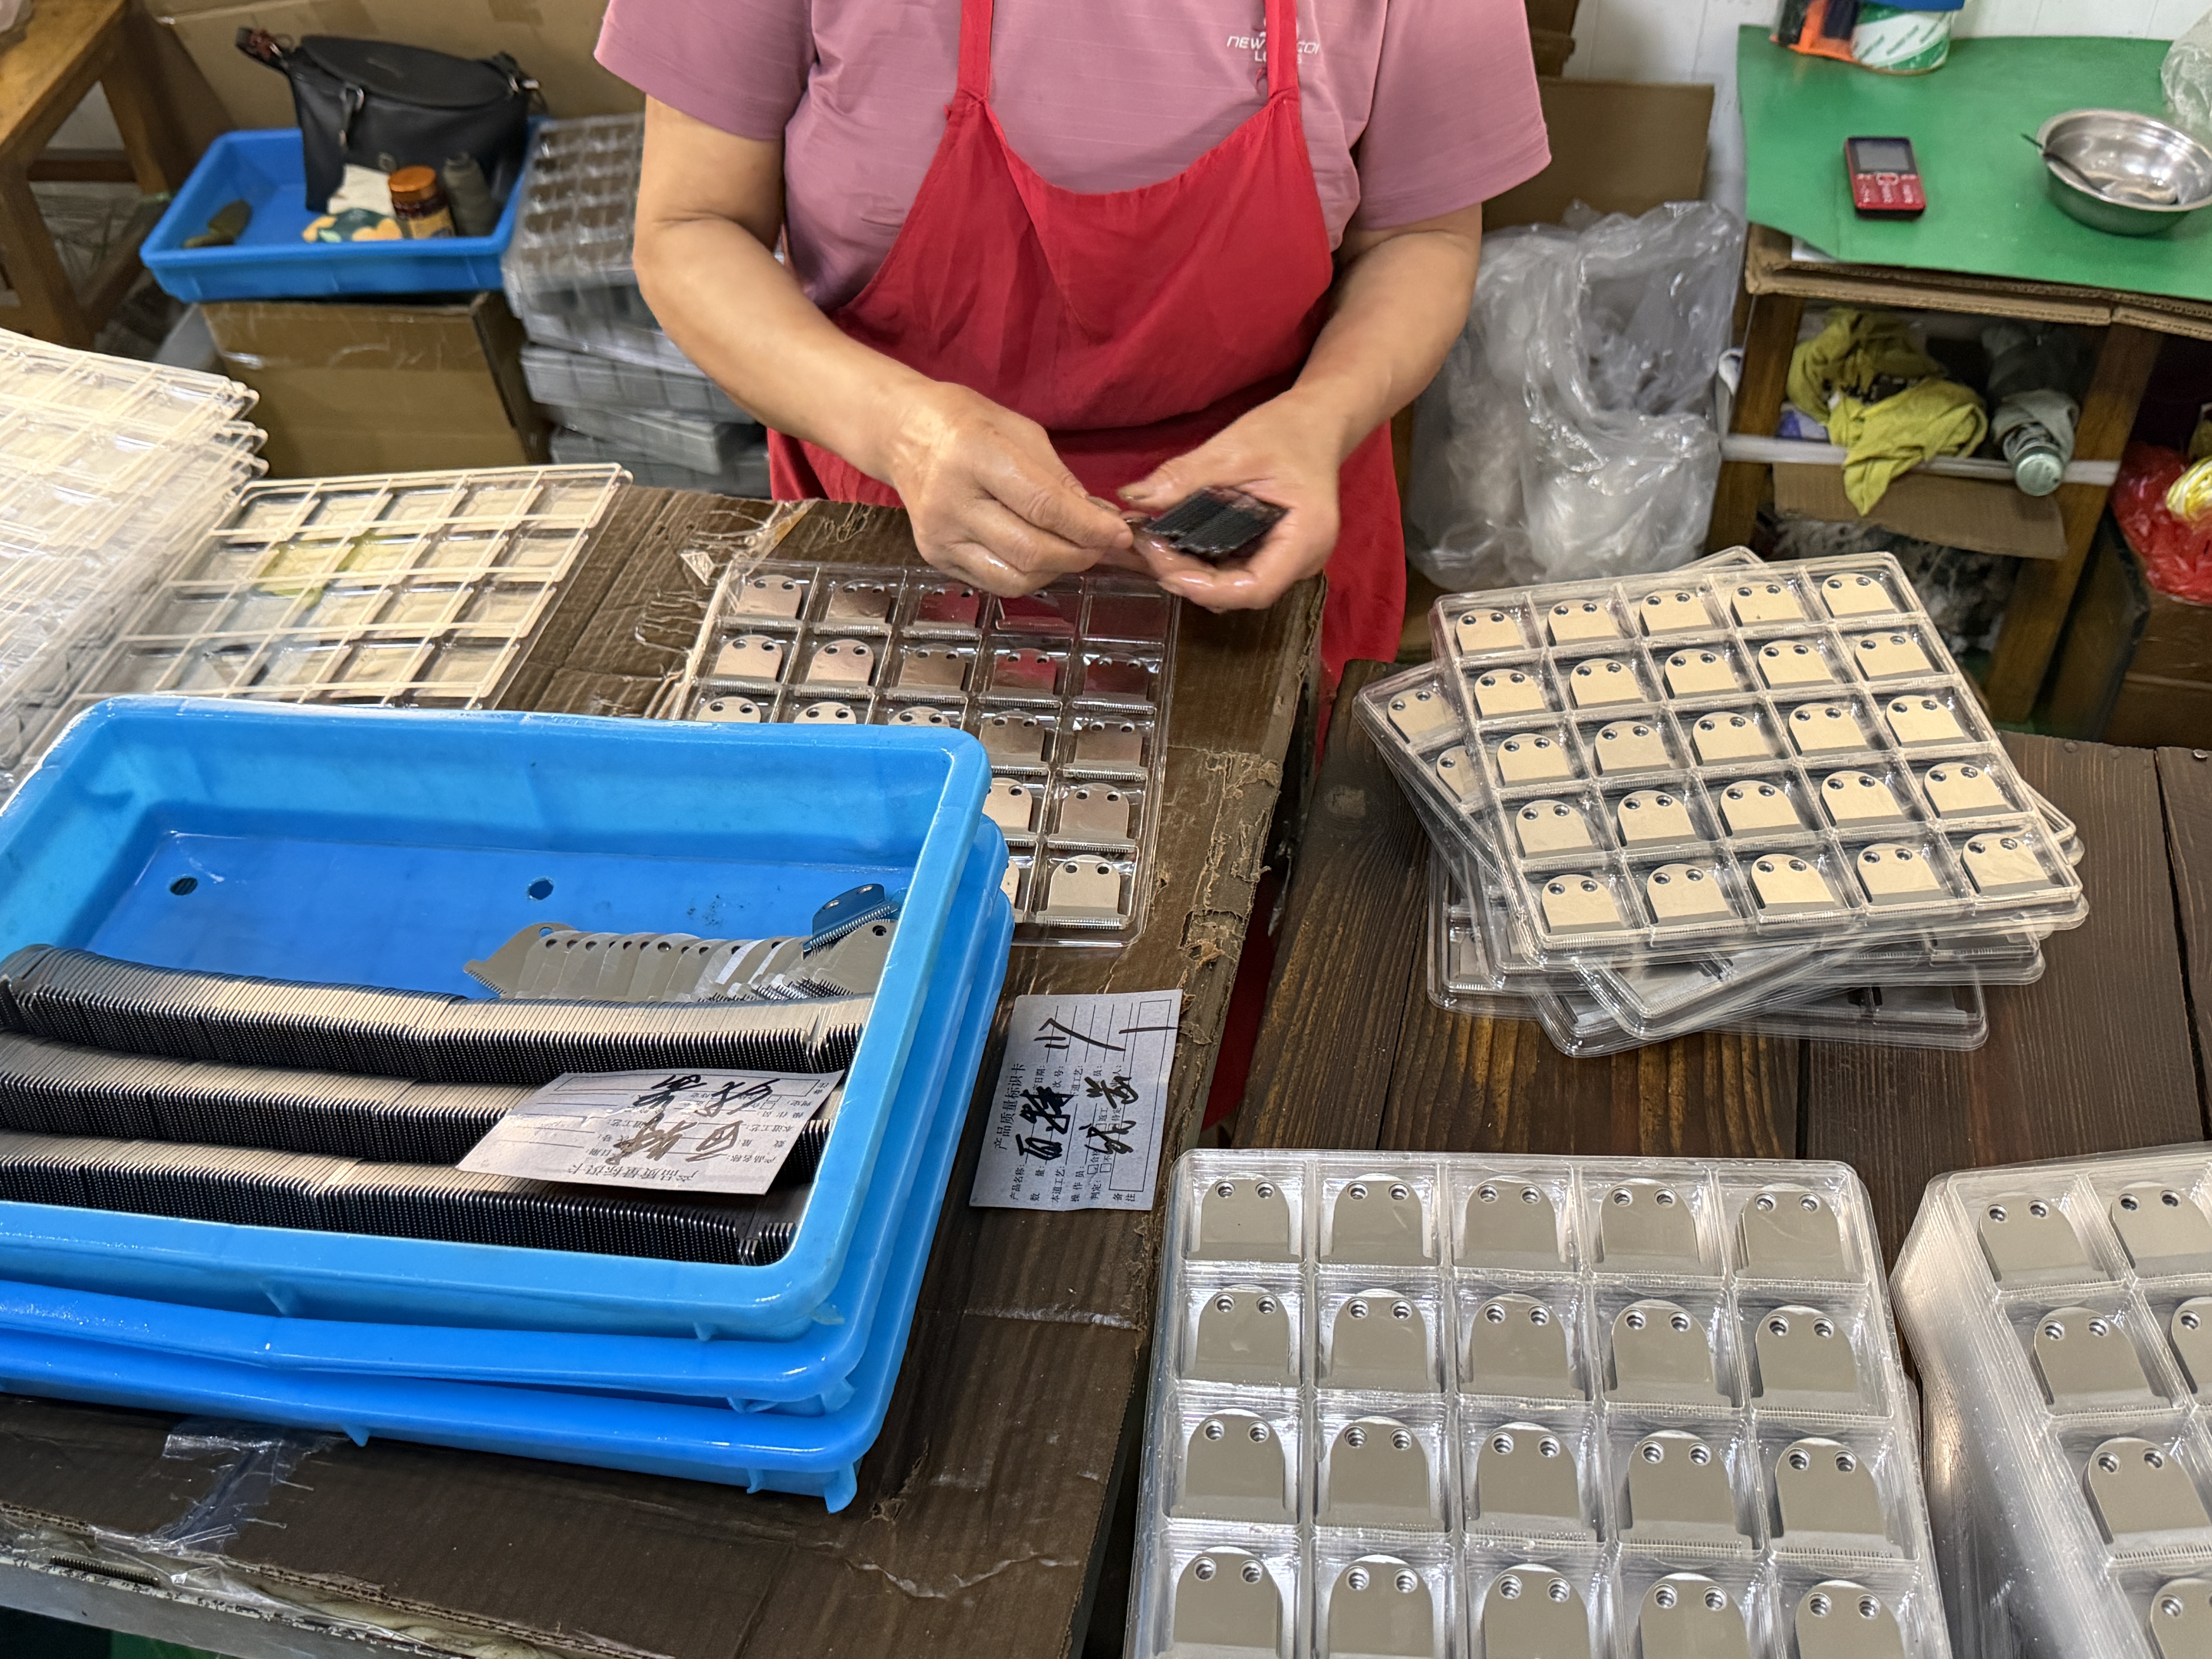
Steel blades rarely fail by breaking. They fail by dulling early, pulling hair, running hot or rusting in the carton. Your inspection plan should target those four outcomes.
- Microhardness on sampled blades (5 pcs per lot). Catches the mesh-belt furnace problem described above. Anything under HV 620 on a 440C blade means heat treatment was skipped or done badly.
- Flatness check (10 pcs per lot). Optical flat or granite plate. This one test predicts most "blade pulls hair" complaints.
- 100% cut test. Every finished set should be run on a host clipper against a standard hair or fibre swatch before packing. Ask whether this is 100% or sampled — at our plant it is 100%.
- Salt spray spot check (3 pcs per lot). 24 hours per ASTM B117. Catches skipped passivation and contaminated grinding coolant, the two usual causes of carton rust on sea shipments.
- Host-clipper fit test. For A5 blades, test the latch on at least three host models (for example Oster A5, Andis AGC and Wahl KM10). A blade can pass every dimensional check and still rattle on one brand's hinge.
For the final random inspection, ISO 2859-1 General Inspection Level II with AQL 1.0 for major defects and 2.5 for minor defects is the norm in this category. Define "major" in writing: a missing or chipped tooth, a failed cut test, visible rust or a failed fit are major. A cosmetic scratch outside the tooth zone is minor.
Six Red Flags When Auditing a Stainless Steel Blade Factory
- No grade on the quote. Covered above. It is almost always 3Cr13 or 4Cr13.
- No heat treatment in-house and no named subcontractor. Outsourcing is fine; not knowing where it happens is not.
- HRC quoted without a test method. On a thin blade, a bare "HRC 60" figure should prompt the question "measured how?"
- Lapping done on a single shift by one operator. Grinding and lapping take the most labour. A factory where one person laps an entire day's output is sampling, not lapping.
- Samples far better than production. Ask for samples pulled from a running production lot, not made by hand in the toolroom. Keep one sample sealed as your golden reference.
- A trading company showroom presented as a plant. Ask for a live video walk from the furnace to the packing line. Our list of verified clipper blade manufacturers in China explains how to tell the difference.
Stainless Steel or Ceramic? Deciding Before You Tool Up
Many buyers arrive asking for stainless steel and leave with a hybrid set, or the reverse. The deciding factors are the end user and the price point, not which material is "better". Stainless steel is the right answer for the stationary blade in every case, for barber blades below about $25 retail, and for any blade the end user will resharpen. A zirconia moving blade earns its 2.2-3.5x cost premium in high-volume pet grooming, where heat and continuous run time are the complaints. The ceramic side of this decision is covered in our ceramic clipper blade manufacturer guide. The full material comparison, including carbon steel and coatings, is in ceramic vs stainless vs carbon steel.
Working With Us
SUMTHIN has run stamping, MIM, vacuum heat treatment, grinding and lapping under one roof in Yanguan Industrial Park, Haining since 2004, with 360 staff and ISO 9001:2015 and ISO 14001:2015 certification audited annually. We supply finished blade sets and loose blades for professional barber clippers, A5 detachable blades and pet and livestock blades. Catalogue samples ship within 7 days, and we will fill in the ten-line spec sheet above for any blade we quote.
Related Guides
- Clipper Blade Steel Grades Explained — 420, 440A, 440C and carbon steel for end users
- How Clipper Blades Are Made: MIM Process — all 18 steps from powder to packed blade
- Ceramic Clipper Blade Manufacturer Guide — zirconia grades, CIM tooling and ceramic pricing
- Detachable vs Fixed Clipper Blades — which blade architecture to design your clipper around
- How to Start a Clipper Blade Brand — private label and wholesale sourcing step by step